
A picker walking an extra 20 metres for every order line may not look like a major problem. Across thousands of lines each week, it becomes lost capacity, rising fatigue and delayed despatch. Knowing how to optimise pick faces is therefore not simply a storage exercise. It is a practical way to reduce travel, improve pick accuracy and make better use of the people and space already available.
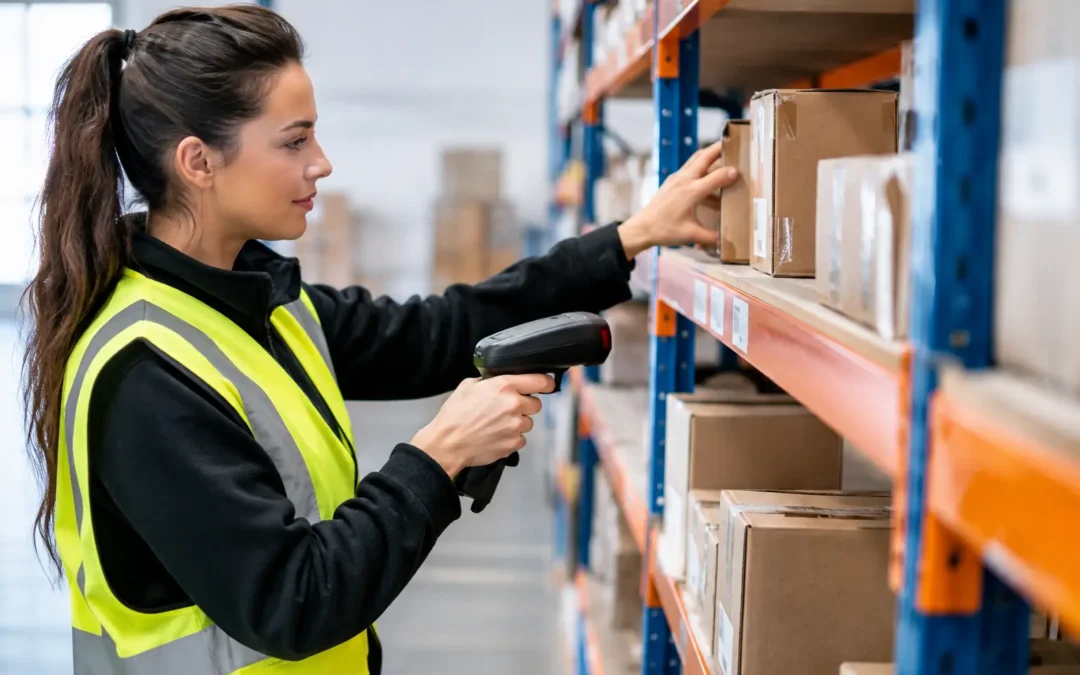
A pick face is the location from which an operative normally picks an item for an order. It may be a shelf bin, carton-flow lane, pallet position or automated storage location. The best arrangement places the right stock, in the right quantity, in the right location for the demand it receives. The detail matters because a fast-moving item with an undersized pick face creates constant replenishment work, while a slow-moving line in a prime location consumes valuable space.
Start with demand, not assumptions
The first step is to understand what is actually being picked, rather than where items have historically been stored. Warehouse teams often inherit layouts shaped by supplier delivery patterns, product categories or the preferences of a previous operation. Those rules can be useful, but they are not a substitute for current order data.
Review at least three to six months of order history, allowing for seasonal peaks where relevant. Identify each SKU’s pick frequency, units picked, order-line frequency, average quantity per line and physical characteristics. An item picked once per order but in large quantities may need a different location and replenishment method from an item picked frequently in singles.
ABC analysis is a sensible starting point. A-items account for a high proportion of picks and should normally sit in the most accessible zones. B-items require good access but do not need the same premium space. C-items can be positioned further away or at higher and lower levels, provided their location does not create a safety or handling issue.
However, ABC categories alone can oversimplify the operation. Demand can change by channel, customer, day of week and season. A product that is slow moving for wholesale orders may be a frequent single-unit pick for direct fulfilment. Your slotting rules need to reflect the work being released to the floor, not just annual sales volume.
How to optimise pick faces using slotting rules
Once demand is clear, create rules that determine which products belong in the primary pick area and how much stock each face should hold. This turns slotting from a one-off tidy-up into an operational discipline.
The most useful rules balance four factors:
- Pick velocity – how often the SKU is accessed.
- Cube and handling profile – its dimensions, weight, shape and whether it is picked as singles, cartons or pallets.
- Affinity – items commonly ordered together.
- Replenishment effort – how often reserve stock must be moved into the pick face.
Place fast movers within the shortest practical travel path, typically in the golden zone between knee and shoulder height. Heavy products should be located at lower levels, while lightweight, small-volume lines can use higher shelves where appropriate. Do not force every popular item into the same aisle if doing so creates congestion. High-demand products may need to be spread across zones, particularly where multiple pickers work simultaneously.
Product affinity is often overlooked. If two items repeatedly appear on the same order, storing them close together can reduce travel. There is a trade-off: grouping related items too tightly can create traffic at the same locations during busy waves. A warehouse management system can reveal both the affinity opportunity and the congestion risk by analysing order patterns and picker movement.
Size each pick face for the real replenishment cycle
An optimised pick face must hold enough stock to support efficient picking without being so large that it wastes space. The aim is not to eliminate replenishment completely. It is to make replenishment planned, safe and proportionate to demand.
Calculate the required capacity from average demand over the replenishment interval, then add a sensible buffer for variation. For example, if a SKU is picked at 120 units per day and the team replenishes every four hours, the pick face needs at least 40 units for expected demand during that period. The final capacity should also account for a safety buffer, case pack quantity and the space required for clear stock rotation.
A carton-flow lane may be ideal for a fast-moving, single-unit product, whereas a full-pallet pick face is more appropriate for bulky cases. The wrong storage medium can undermine an otherwise sensible layout. Small items in deep pallet locations increase reaching and searching; bulky cartons in narrow shelving can slow every pick and increase damage risk.
Minimum and maximum stock settings should be maintained in the WMS, not held in a spreadsheet or remembered by supervisors. When the system knows the active pick-face capacity, on-hand quantity and expected workload, it can generate replenishment tasks before the face is empty. This avoids the familiar disruption of a picker stopping mid-order to find stock elsewhere.
Separate replenishment from picking where possible
The best slotting plan can still fail if forklifts and pickers compete for the same aisle at the same time. Replenishment should be designed around the picking operation, not treated as an afterthought.
Where volume permits, schedule bulk replenishment before waves are released or during lower-activity periods. For continuous operations, use directed replenishment tasks that consider the next wave, reserve-stock location and travel path. This helps avoid reactive replenishment, which is usually more expensive and more disruptive.
There will be exceptions. Promotional demand, late inbound deliveries and volatile product ranges may require top-up replenishment during active picking. In those cases, clear aisle controls, task priorities and vehicle segregation are essential. Speed is valuable, but it should not compromise safe movement or stock accuracy.
Design around the picking method
Pick-face optimisation is closely tied to how orders are picked. A layout suited to single-order picking may perform poorly when the operation moves to batch, cluster or wave picking.
For batch picking, group high-frequency small items in compact zones so an operative can collect multiple order quantities in one pass. For zone picking, make sure each zone has a balanced workload. There is little benefit in shortening travel in one area if another zone becomes the constraint that holds orders back.
Wave picking introduces another consideration: the profile of each wave. If all priority orders contain the same fast-moving lines, a single aisle can become a bottleneck. A WMS can apply allocation and wave rules that smooth demand, split work across locations and release replenishment early enough to protect throughput.
Keep stock accurate before moving stock around
Slotting decisions are only as good as the inventory data behind them. If a pick face shows stock that is physically absent, the picker still has to search, substitute or raise an exception. That damages the intended benefit of an optimised layout.
Use directed putaway to ensure replenishment stock is placed in the correct reserve location, and confirm every movement by barcode scanning or suitable RFID processes. Cycle counting should focus attention on fast-moving pick faces because errors in these locations have the greatest effect on service and labour. Check location labels, unit-of-measure rules and pack conversions as well. Many apparent stock problems are caused by a mismatch between eaches, inner packs and cases.
A clear location naming convention also matters. Operatives should be able to identify aisle, bay, level and position quickly, without interpreting inconsistent labels. This is particularly important for temporary labour and new starters during peak periods.
Measure whether the new layout is working
Do not judge an optimisation project by how tidy the warehouse looks after a re-slot. Measure the operating result over several weeks, comparing like-for-like demand periods where possible.
Useful indicators include picks per labour hour, average travel distance or time per line, replenishment tasks per 1,000 picks, short picks, pick errors and order cut-off performance. Also watch congestion. A faster average pick time can conceal long delays at a few pressured aisles.
Warehouse intelligence should make these measures visible by zone, picker, SKU family and shift. That allows managers to distinguish between a layout issue, a replenishment issue and a training issue. It also prevents a major slotting change being driven by a single difficult day.
Treat pick-face optimisation as a routine
Demand, product ranges and order profiles do not stand still. A location plan that works well in January may be inefficient by September, particularly after a new customer win, range extension or channel change. Review A-items frequently and conduct a wider slotting review at planned intervals, with additional checks before peak trading periods.
For businesses managing complex picking, a configured WMS provides the control to turn demand data into directed tasks, active replenishment and measurable labour performance. Smarter Warehouse helps operations teams connect those capabilities to the realities of their layout, equipment and order profile.
The most effective improvement is usually not a dramatic warehouse redesign. It is a disciplined cycle of analysing demand, setting practical location rules, protecting stock accuracy and adjusting before small inefficiencies become daily friction.